Capability 04 — Manufacturing
The last ten percent of quality is decided on the line.
A good prototype does not prove a production process. What proves it is a defined test at every gate, a fixture that measures the same thing every time and a record that ties a shipped unit back to its lot.
Production floor
The line you audit is ours.
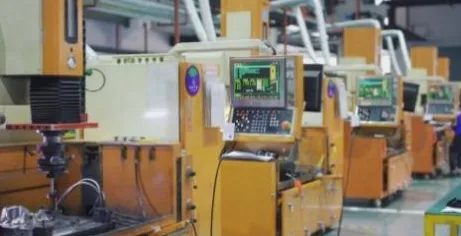
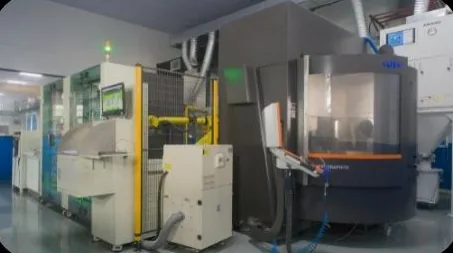
Serow runs its own manufacturing center: a tool room, injection molding, SMT, silk-print and twelve remote-control assembly lines. A tooling change does not wait in an outside factory’s queue.
The largest line group on site.
In-house tool room capacity.
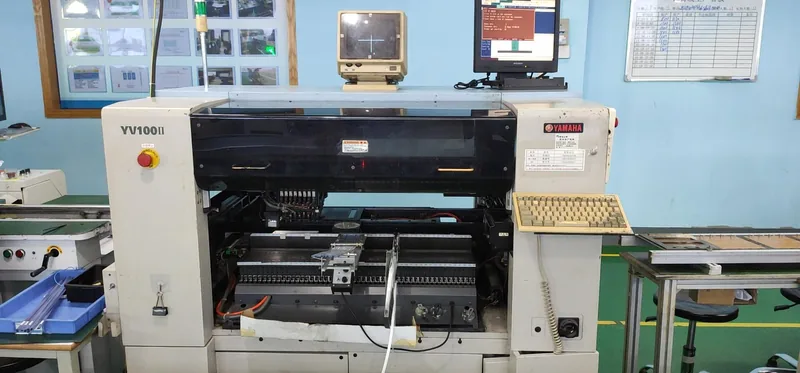
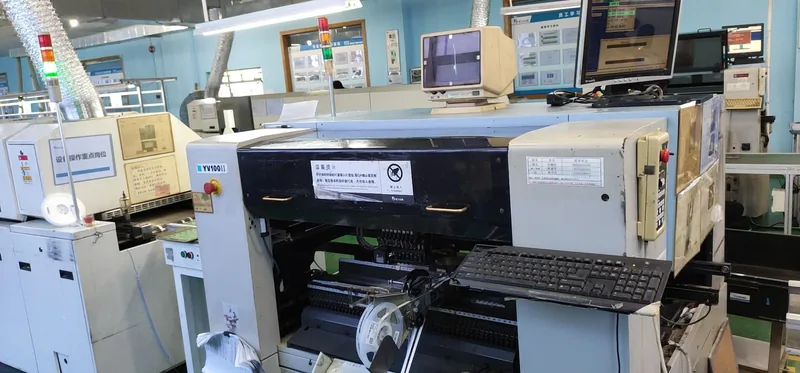
YAMAHA YV100II, supporting our own boards.
Sub-assembly and final build.
| Process | Lines | Note |
|---|---|---|
| Remote-control assembly | 12 | Final build, test and pack |
| General assembly | 6 | Sub-assembly and accessories |
| Ultrasonic welding | 5 | Housing sealing |
| Laser | 4 | Laser machines |
| Silk printing | 2 | Legends and decoration |
| SMT | 3 | YAMAHA YV100II |
| Tooling | 100 / year | In-house tool room |
SMT is a supporting process for our own boards; the volume business is assembly, tooling and test.:
Production flow
Five gates between components and a sealed carton.
Each gate has an accept criterion and a record. A unit that fails a gate is quarantined, not reworked quietly and returned to the same lot.
Incoming inspection
Components, PCBs, keypads and housings are checked against the approved sample and drawing. Critical items — radio module, crystal, battery contacts, keypad material — are checked per lot.
SMT and board test
Boards are assembled, reflowed and inspected. A board-level test checks power, key scan, IR output and radio transmission before assembly into the housing.
Final assembly
Keypad, board, battery contacts and housing are assembled on a defined fixture. Sealing, screw torque and battery-door fit are checked against the work instruction.
Functional test
Every unit is tested for key function, IR output, radio range and current draw. Units are tested with the firmware version released for that order, not a generic build.
Packaging and traceability
Accessories, labels and language variants are checked against the order. The carton label carries the lot, quantity and firmware version so a field issue can be traced back.
Inside the line
Quality gates
What is measured, and with what.
| Check | Method | Frequency | Record |
|---|---|---|---|
| Key function | Fixture presses every key; receiver confirms code | Every unit | Per-unit pass/fail |
| IR output | Receiver or optical sensor confirms carrier and frame | Every unit | Per-unit result |
| Radio range | Fixed-distance test through the final housing | Every unit or sampled per lot | Test log |
| Current draw | Sleep and active current against the approved limit | Sampled per lot | Measurement record |
| Housing fit | Gap, flush and battery-door check against the limit sample | Sampled per lot | Visual inspection sheet |
| Sealing | Program-specific test when an IP target applies | Per validation and sampled in production | Test report |
Sampling levels and accept criteria are agreed in the production test specification. They are not left to the operator’s judgement on the day.:
Traceability
When a fault occurs at the customer site, we trace it to the batch rather than to guesswork.
Every order carries a lot record: component lots, firmware version, test fixture, test results and packing list. When a unit fails at the customer site, the record narrows the question to a specific batch instead of the whole product history.
For configured products, the record also includes the configuration file — key map, language set and property code — so a replacement can be matched to the original.
- Packing list with lot and quantity
- Firmware version and configuration reference
- Functional test summary
- Approved sample retained for reference
- Certification copies for the shipped model and market
Capacity
We schedule line time per program — it is not a price-list slot.
A headline monthly capacity is meaningless if your program shares a line with three others during peak season. We confirm the allocation for your order window before you commit to a launch date.
Pilot builds are scheduled with the same fixtures that will run mass production, so the process is proven before volume. If a fixture cannot keep up, we find that out on the pilot, not in the first shipment.
Questions
Manufacturing FAQ
Can we audit the line or the test records?
What happens when a unit fails functional test?
Do you test every unit’s radio range?
Can production move to another site later?
Start a project
Ask for the test specification before the price.
The test specification tells you what the unit price actually buys. We would rather discuss that first.